

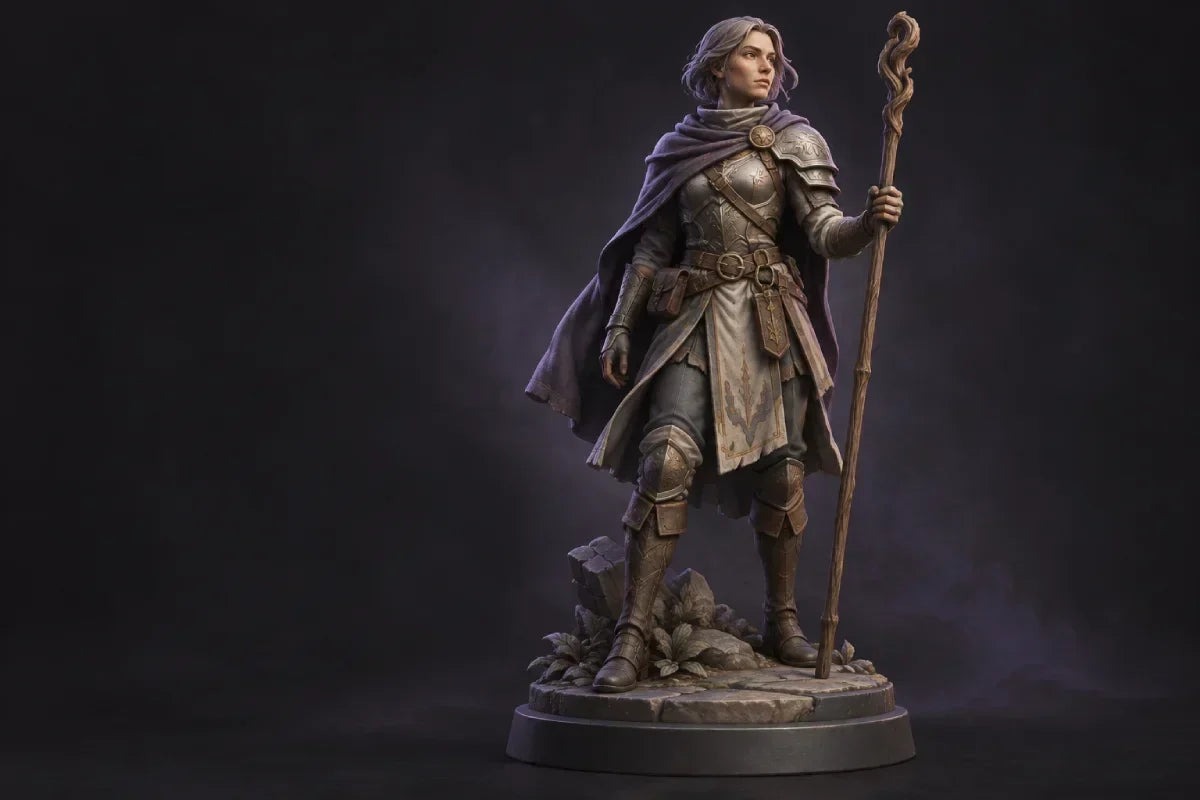
High-detail resin miniatures come from a chain of small decisions: a sound model at the intended scale, a compatible printer and resin profile, an orientation that supports the important surfaces, a checked layer preview, and material-specific washing and curing. The most useful habit is to pause at each handoff and inspect what the next stage will inherit. Auto tools can speed preparation, but they do not tell you whether a contact mark lands on a face or whether a thin blade has a sound path through the supports.
This guide focuses on those checkpoints. It uses the HeyGears Reflex RS Turbo as one workflow example; the same concepts apply broadly to resin miniature printing, while settings and device actions remain model-, printer-, and resin-specific. HeyGears already publishes a broad first resin print workflow. This guide concentrates on how to catch detail risks at each step and when to go back and revise.

The support-removal and curing sequence depends on the exact resin instructions.
Detail is more than a small layer height
Resin printers build a model from thin cured layers, but the layer-height number is not a promise that every feature of that size will reproduce cleanly. XY pixel size describes the projected image sampling across the build plane; layer thickness describes the vertical step between layers. They are different machine specifications, and neither alone describes the final accuracy of a miniature. The RS Turbo product page, for example, lists a 29.7 μm XY pixel size and a 30–100 μm layer-thickness range as separate specifications. Resin behavior, exposure profile, feature orientation, support contacts, and the sculpt itself also affect the result.
Start with the feature you need to keep: an eye ridge, chain, finger, blade edge, or engraved line. If that feature is missing or too shallow in the source mesh at the intended print scale, choosing a smaller layer height cannot restore geometry that is not there. If the feature exists digitally but sits across a broad stair-stepped surface, orientation and layer stepping may matter more than reducing the layer height alone.
1. Check the STL at the size you intend to print
An STL file describes the model's surface as triangles; the slicer turns that surface into layers. Before adding supports, import the file and inspect it at the final miniature size. Check that the model is the intended scale, fits the build area, and has not imported with a missing part, open seam, inverted-looking face, or disconnected shell. If your slicer flags a mesh problem, inspect the repaired preview instead of assuming an automatic repair preserved every thin feature.
Zoom in on fragile details and compare them with the original sculpt. Look for blades or straps that nearly disappear, fingertips that merge into a weapon, and cloth edges that are thinner than the intended resin and process can reliably preserve. A useful correction may be to print larger, choose a sturdier version of the model, or accept that a tiny feature will be simplified. Do not try to solve a geometry problem by changing exposure blindly.
If the miniature is hollowed or contains a deep cavity, inspect that cavity in the slicer too. A cup-like shape can trap resin or create suction during a peel cycle. For a hollow model, verify that the chosen hollowing and drain openings actually connect to the cavity and remain accessible after orientation. If you cannot confirm that, use a solid model or return to the design step rather than printing a sealed pocket full of liquid resin.
2. Match the printer, resin, tank, and profile
In the slicer, select the exact printer and resin combination available for your job. Confirm the material name, tank or build configuration, and profile shown in the project before you slice. A profile is a material-and-device starting point, not a generic “miniature” preset: exposure and motion settings depend on the resin and printer combination.
For a first job with a supported HeyGears resin, begin with its current fine-tuned Blueprint Studio profile. HeyGears describes these profiles as the lower-setup path. Its Open Material Mode provides adjustable settings and is aimed at experienced users testing and tuning their own process; the RS Turbo can use compatible third-party UV-curable resins in that mode. “Compatible” matters: this is not a guarantee that every resin will work or that another resin's settings can be copied unchanged. Check the current compatibility and resin instructions before committing a model.
Choose layer thickness using the resin profile and the needs of the model. Finer vertical steps can make sloped surfaces appear smoother, but they also increase the number of layers. They do not fix unsupported islands, weak contacts, or undersized sculpted details. Change one process variable at a time and keep a note of the resin, profile, layer setting, and model revision so you can interpret the next print.
3. Orient for both geometry and the surfaces you want to keep
There is no one best miniature angle. Rotate the model while watching its layer cross-sections. A useful orientation avoids a sudden jump from a tiny island to a broad cross-section when possible, keeps long unsupported spans manageable, and gives delicate branches a stable route back to the raft or platform. Hollow or cup-shaped sections need special attention because their orientation can trap resin or air.
At the same time, decide which surfaces matter most after painting. Faces, armor engravings, cloth texture, and visible weapon edges are poor places for avoidable support contacts. Orient those presentation surfaces away from supports where the geometry allows. The choice is a tradeoff: moving contacts can create a longer lever or unsupported area elsewhere, while adding too many contacts can scar details and make cleanup harder.
Use auto-orientation or auto-supports as a first pass, then rotate the model and inspect it from underneath and behind. Check the first point of every isolated feature, including fingers, horns, sword tips, cloak points, and the underside of the base. If an island starts in midair, add a support or revise the orientation. If a support tip sits on an important detail, move it to a less visible, stronger area when possible. There is no universal support diameter or contact depth: use the profile and slicer controls for your printer and resin, then inspect the result at magnification.
4. Read the layer preview before sending the job
The 3D view can hide a problem that is obvious one layer at a time. Scrub the preview from the raft upward and ask:
|
Check |
What to look for |
If it fails |
|
First appearance |
Does each separate part of the miniature begin on the raft, a support, or an already printed section? |
Add a support or reorient the model so the feature grows from a connected structure. |
|
Delicate details |
Do blades, fingers, horns, and cloth tips remain connected as their cross-sections appear? |
Strengthen the path or revise the model; do not rely on a floating first layer. |
|
Sudden broad layers |
Does a large area appear abruptly, or do separate branches merge into a broad section? |
Reorient to reduce the abrupt change where practical, then review supports and the updated preview. |
|
Contact placement |
Are supports landing on the face, raised relief, or a thin edge you need to keep? |
Move the contact if possible and preview again. |
|
Hollow geometry |
Are cavities open to a drain path and oriented so liquid resin can escape? |
Revise the hollowing/orientation or print solid if you cannot verify drainage. |
|
Job selection |
Do the printer, resin, profile, scale, and build area match the intended job? |
Correct the project settings before slicing or sending. |
Do not treat a completed slice as proof that the file is ready. If you change orientation or supports, regenerate and reread the preview: the correction can move the first appearance of a feature and create a new unsupported region.

Illustrative cross-sections only; they do not prescribe a universal angle or support size.
5. Send the checked job, prepare the printer, then use a stop rule
Before opening or handling resin, read the SDS for the exact material and prepare the PPE, ventilation, spill response, and waste handling it specifies. Keep uncured resin off skin and out of food areas. If resin contacts skin or eyes, follow that SDS rather than improvising a cleanup method.
Once the preview passes, slice the project and send or transfer the job through the supported Blueprint Studio workflow for the selected printer. At the machine, verify that the displayed job and material match your project. Seat the correct tank and build platform, check for cured debris, and add or confirm resin using the instructions for that printer, tank, and material. Start the job through the machine's current documented controls. The HeyGears support page is the entry point for documentation and help; select the exact model. A Reflex RS guide is not automatically a Reflex RS Turbo guide, so do not transfer model-specific loading or removal steps between them.
Stay available for an error or abnormal event, but do not reach into a moving printer or bypass an interlock. Stop and inspect before the next job if the machine reports a failure, the build is visibly incomplete, a platform does not appear to have formed the expected part, or you suspect cured debris may remain in the tank. Follow the exact printer's cleanup procedure before restarting; a new job can press debris into the release surface or contaminate the next print.
The RS Turbo can remove several setup tasks from this step: the product page lists floating-screen auto leveling and automatic resin refill. Automatic resin heating is listed with the separately purchased RS Heated & Pulsing Release Resin Tank. These features reduce particular manual steps; they do not inspect the mesh, approve supports, confirm resin compatibility, or replace the material's safety and processing instructions. Check your actual package and installed tank before assuming a feature is present.
6. Wash, dry, and finish in the order specified for your resin
When the job is complete, follow the exact printer's instructions to let excess resin drain and to remove the build platform safely. Keep the miniature on its supports during transfer, let it drip over the protected resin area, and move it carefully to the wash station. Wear the SDS-specified PPE and avoid carrying uncured resin across clean surfaces. Inspect the supported miniature before washing: confirm that fragile pieces are present and attached, and that there is no obvious shift, torn area, or missing limb. If the build failed or a cured piece may have detached into the tank, stop and follow the device's failed-print inspection and cleanup procedure before printing again.
Wash with the liquid and process specified for the exact resin. The goal is to remove uncured surface resin from recesses, undercuts, and support junctions without soaking longer than the material guidance allows. Inspect deep folds, the underside of the base, and gaps between supports. If you still see residue, follow the resin maker's rewash guidance; do not assume that a shiny surface has one cause or compensate with extra curing.
For a hollow miniature, use the resin maker's applicable process to wash the interior through its drain openings. Check that wash liquid can reach the cavity and that uncured resin and solvent can drain back out. Formlabs' general washing guidance notes that hollow parts can retain solvent, air, or uncured resin and says to let solvent drain into the wash container before transferring the part. HeyGears' troubleshooting guide also discusses drain openings as a way to wash internal uncured resin. These sources support the need to inspect and drain a cavity; they do not establish a HeyGears-specific wash method or universal hole layout. If liquid or residue remains inside, return to the material-appropriate rinse/flush and draining step. Do not move the part to drying or curing until the interior is clear and drained.
Let the miniature dry completely before post-curing. A damp or solvent-wet surface is a reason to wait and check again, not a cue to start the cure cycle. Follow the exact resin's processing instructions for whether supports stay on during curing or are removed beforehand, then use its cure profile. There is no universal support-removal order: recommendations differ by resin and workflow. For fragile fingers or weapons, use a suitable flush cutter and support the part near each cut so the force does not travel through the thin feature.
After curing, inspect the model under a bright, angled light. Look for support scars, blocked recesses, missing details, tacky areas, cracks, and deformation. Do not use appearance alone as your cure check; follow the material's cure instructions and inspect the actual part. If its surface remains tacky or an area looks underprocessed, check the material guidance before handling it further or priming it. Only sand a fully processed part, and use suitable protection to avoid breathing dust.
For solvent handling, use the solvent supplier's SDS. IPA is flammable, so keep it away from ignition sources and store it in a suitable closed, labeled container. Do not pour liquid resin or resin-contaminated wash solvent down a drain or into household waste. Follow local hazardous-waste rules for resin, contaminated wipes/gloves, and used wash liquid; disposal options depend on location.
What the RS Turbo changes in this workflow
For a compatible HeyGears material, the standard profile in Blueprint Studio is the simplest starting point because the device and material are represented in the supported preparation workflow. The RS Turbo page also lists auto leveling and automatic resin refill. If the separately purchased heated and pulsing release tank is installed, automatic resin heating is another available step. Experienced users can use Open Material Mode for compatible third-party UV resins and their own validated settings. After slicing, Blueprint Studio provides the supported route to transfer the prepared job; machine-side loading, starting, draining and platform removal still follow the instructions for the exact Reflex RS Turbo setup.
Those are specific reductions in manual setup and profile friction. They do not make the printer a one-click guarantee: file scale, support placement, layer-preview review, material-specific post-processing, and cleanup remain part of the job. If you are comparing machines for this workflow, check the current Reflex RS Turbo specifications and package options, including whether the heated tank is included in the configuration you are considering.
A repeatable detail check
For a new miniature, keep a short record of the STL version and scale, printer, resin, profile, layer thickness, orientation, support changes, and post-processing profile. When a feature is lost or scarred, compare these notes with the layer preview and contact locations before changing exposure or adding supports everywhere. That gives the next revision a clear question to answer: did the detail disappear in the source geometry, fail to connect during printing, get damaged during cleanup, or change during post-processing?
That checkpoint-based approach makes miniature printing easier to repeat. You catch the issue at the stage that created it, preserve the details that matter to the sculpt, and carry only a verified part into the next step.
Share:
How to Reduce 3D Printing Waste: Resin, Supports, and Failed Prints?